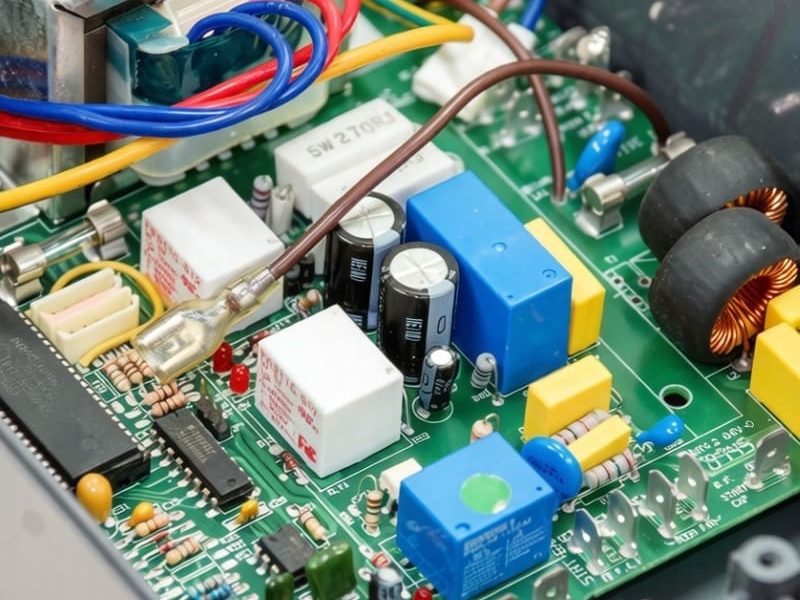
High mix, low volume pcb assembly Manufacturing work rewards manufacturers who can move fast without losing their grip on quality. The real challenge is holding variety, quality, cost and delivery in balance when no two orders look alike. Success here is not about working harder; it comes from designing the whole operation around change: clear processes, people who can adapt, equipment that bends instead of breaks, and enough visibility that teams can act before a small problem turns into a bad week.
What is high mix low volume manufacturing?
High mix low volume manufacturing is a way of producing many different products, variants or configurations in relatively small quantities. Rather than running one job for weeks on end, teams switch constantly between orders, materials, instructions, tooling and quality requirements. You see it wherever customers need something tailored instead of pulled off a shelf: custom manufacturing solutions, specialized components, engineered products, prototypes and replacement parts.
The payoff is responsiveness. Customers get boards and assemblies that actually fit their design, and the manufacturer serves niche demand without betting the whole schedule on a single large run. The cost of that flexibility is friction. Every changeover carries setup time, the risk of an outdated drawing, a scheduling scramble, or a quality gap that only shows up late. A good strategy is simply a way of turning that friction into a rhythm the shop can live with.
The real challenge is complexity, not volume
In low volume production, the part count is rarely the hard part. Variation is. A small shop may build far fewer units than a high-volume plant, yet juggle many more part numbers, bills of materials, routing paths, inspection plans and customer-specific notes.
That complexity quietly eats performance if you let it. People lose hours hunting down the right revision, confirming details, staging the wrong material or waiting on an approval. Machines idle through setups while planners try to squeeze an urgent custom job into a schedule that is already moving. Treat high mix low volume manufacturing like standard, repetitive production and you build inefficiency straight into the working day.
The fix is to design for change from the start. Assume orders will vary, instructions will get updated and schedules will slip. The aim is not to kill variation, because in this business you cannot. The aim is to make variation visible, repeatable and easier to control.
Build flexible systems around the work
Flexible manufacturing systems is not just a story about robots and automation. It is about building an environment that adapts without forcing people to rebuild the process every time a new job lands. In a high mix shop, flexibility has to show up in the equipment, the workflow, the people, the software and the way decisions get made.
In practice a flexible system leans on modular workstations, quick-change tooling, cross-trained operators, digital work instructions and production data that is genuinely easy to reach. When those pieces line up, the floor moves between jobs with far less confusion and far less waiting.
A few concrete places to start:
- Standardize what you can. Even fully custom work can share common setup steps, inspection checkpoints, labeling rules and documentation formats.
- Use modular tooling and fixtures. Reusable fixture elements mean you are not inventing a new setup from scratch on every order.
- Keep work instructions current and visual. Photos, diagrams, revision notes and plain acceptance criteria let operators move between products with confidence.
- Cross-train on purpose. A broader skill base gives planners more options when priorities shift or a key person is out.
- Group similar jobs where you can. Families of parts that share materials, tools or processes can cut changeover time noticeably.
Flexibility is not the same as improvising all day. It is a dependable framework that still leaves room to change.
Planning small batch production with fewer surprises
Small batch production is profitable and efficient when planning reflects what short runs really feel like. Jobs move through the facility fast, which leaves weak planning very little time to correct itself. Missing material, an unclear drawing or a fixture that is out for maintenance can stop everything the moment the job reaches the floor.
Strong planning begins before the job ever hits the shop. Teams confirm the latest customer requirements, the materials needed, the inspection steps, available machine capacity and any special handling. That front-end discipline keeps production from becoming the place where incomplete information finally comes to light.
A practical pre-production checklist is not glamorous, but in low volume high mix work the basics are what create stability:
- Confirm the current revision. Drawings, specifications and instructions must match the order that was actually accepted.
- Validate material availability. Check quantity, grade, certification, likely substitutions and lead time before the job is scheduled.
- Review tooling and fixtures. Know what is needed, what is shared with other jobs and what is due for maintenance.
- Define quality checkpoints. Decide when inspections happen and what has to be documented at each one.
- Estimate setup effort honestly. On short runs, setup can dominate the job, so plan for it openly rather than hoping for the best.
- Clarify packaging and delivery. Custom orders often come with customer-specific labeling, protection or shipment timing.
When people know what is ready and what is not, they schedule better and avoid stops that were preventable all along.
How can manufacturers reduce changeover time?
Changeover time comes down when you separate the setup work that has to happen while a machine is stopped from the preparation that can happen earlier, standardize the repeatable parts, and have tools, materials and instructions ready before the current job is even finished. The goal is to strip out waiting, searching and rework, not to ask operators to work faster or risk the result.
A simple way to start is to watch one typical changeover and write down every step. Some genuinely require the machine to be idle. Many do not. Materials can be staged, fixtures cleaned, programs verified and inspection tools prepared while the active job is still running.
Most changeover wins come from small, unglamorous changes:
- Store tools and gauges right where they are used.
- Build setup carts for common product families.
- Label fixtures, clamps and adapters clearly.
- Use setup sheets with photos and critical dimensions.
- Tighten the first-article process so approval does not turn into a bottleneck.
- Track the setup problems that keep recurring and remove the cause, not just the symptom.
The best changeover strategy protects quality while it gains speed. In custom work, a fast setup that produces the wrong thing is not a win. What you want is a repeatable setup that helps the team start right the first time.
Quality control has to move upstream
Quality in high mix low volume manufacturing cannot rest on final inspection alone. By the time a small batch reaches the end of the line, there may be almost nothing left to recover in time, material or margin. Quality has to be built into planning, setup, operator guidance and in-process checks.
It starts with clear requirements. If a customer spec leaves room for interpretation, settle it before the work begins. Drawings, tolerances, surface finishes, materials and documentation needs should be easy for the people actually doing the work to understand.
In-process inspection matters especially on small batches. Checking the first piece, verifying critical features during the run, and documenting results at set points can catch a problem before it spreads across the whole order. That is not extra bureaucracy. It is about putting checks exactly where they prevent the most waste.
You can also improve quality by looking at recurring issues across jobs. Even when every order is different, patterns show up. A certain quoting assumption keeps causing pressure late; one product family always seems to trigger inspection delays; a particular handoff keeps producing misunderstandings. Treat those as system problems rather than one-off mistakes, and improvement becomes possible.
Turning variety into better decisions with data
Low volume high mix manufacturing generates genuinely useful information, but only if you capture it in a form you can use. Setup times, scrap reasons, rework causes, routing changes, late materials and inspection results all point to where complexity is quietly costing you money or time.
The trap is trying to measure everything at once. Start with a small set of metrics that feed real decisions. Tracking planned versus actual setup time improves future scheduling and quoting. Watching first-pass yield by product family reveals where instructions or tooling need attention. Recording why schedules slipped shows whether the true constraint is material, capacity, engineering review or quality approval.
Metrics that tend to earn their keep in a high mix shop include:
- Setup time by job type or product family.
- First-pass yield and rework frequency.
- On-time completion by order type.
- Material shortages or late releases.
- Engineering and customer clarification cycles.
- Changeover delays caused by missing tools or instructions.
Data should make conversations clearer, not more complicated. When a team can see what actually happened, it improves the process instead of arguing from memory.
People are still the center of the system
Technology helps, but people are what make a high mix system work. Operators, planners, engineers, quality staff and customer-facing teams each hold a piece of knowledge that affects performance. Keep that knowledge informal and the business ends up dependent on a handful of individuals, and fragile the moment workload shifts.
Cross-functional communication is essential. Planning should understand the constraints production actually faces. Production should have a clear, quick way to ask questions. Quality should be involved early enough to prevent issues, not only late enough to reject work. Sales and customer service should know when a request quietly changes lead time, documentation or cost.
Training matters just as much. In a repetitive environment a person can master a narrow task through sheer repetition. High mix work calls for something broader: better problem-solving, comfort with documentation, and the confidence to stop and clarify when something does not match the plan. Investing in that capability pays off in both flexibility and consistency.
Better quoting protects capacity and margins
A high mix operation can be overloaded without anyone noticing, because quotes tend to underestimate complexity. Low volume work carries a lot of hidden effort: engineering review, programming, special packaging, unique inspection steps, supplier coordination and customer documentation. Miss those early and a job can look profitable on paper while straining the whole shop in reality.
A stronger quoting process looks well past material and run time. It weighs setup effort, risk, inspection needs, revision control and the odds of customer changes, and it uses historical data where it exists, especially for similar product families or repeat customers.
This does not mean every quote has to become slow or heavy. It means the business should know which questions actually matter before it accepts the work. Clear quoting protects the customer too, because the expectations are realistic from the very first email.
A practical path to stronger performance
Improving high mix low volume manufacturing does not require changing everything at once. The most effective approach is usually focused and incremental: pick one area where complexity is causing visible pain, improve it, measure the result, then expand.
A sensible starting list:
- Map one common order path from quote to shipment.
- Identify the top three causes of delay or rework.
- Standardize the handoff between planning and production.
- Improve setup documentation for a single product family.
- Run a simple feedback loop after each difficult job.
- Feed the lessons back into quoting, routing and work instructions.
Every improvement should make the next job a little easier to run. Over time the operation becomes more predictable without turning rigid, and that balance is exactly what a high mix manufacturer needs.
The takeaway
High mix low volume success comes from treating variety as a design requirement rather than an exception. Flexible systems, disciplined planning, clear quality checkpoints, honest data and capable teams all turn genuinely complex work into work that is under control.
Manufacturers who build that foundation can serve specialized demand with far more confidence. They are better placed to handle custom orders, shifting schedules and the small batches that demand precision. In a market where customers increasingly reward responsiveness and tailored solutions, getting high mix low volume manufacturing right is not just a way to cope with complexity. Done well, it becomes a durable competitive advantage.
If you are weighing a high mix, low volume or small batch build, the fastest way to see how this approach fits your board is to send over your Gerbers, BOM and target quantities for a quick review.
Recent Comments